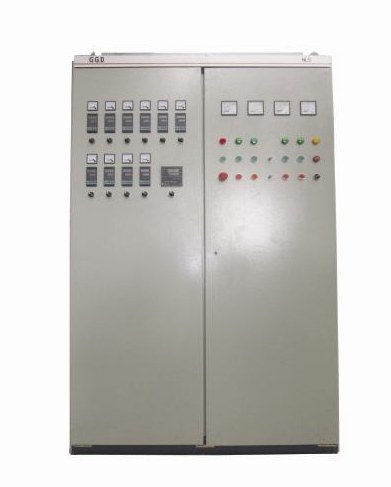
PRODUCTS / PELLETIZING & CONTROL
The pelletizing method and control system define pellet quality and line reliability. We match the cutting and cooling method to your polymer, and specify control and interlocks to protect machine and product.
Strands cooled in a water bath then cut — the workhorse method for filled and reinforced compounds.
Air cooling for compounds that must not contact water, including some cable and heat-sensitive materials.
Cutting at the die face with air cooling for masterbatch and lightly filled compounds.
Die-face cutting with a water ring for uniform pellets on filled systems and blends at higher output.
Control is offered from a standard operator panel through to a simulated panel or full PLC control. Process interlocks for lubrication, feeding, melt pressure and motor over-current protect both the equipment and the product. Temperature control is zoned along the barrel, and the control cabinet is built to your local voltage and frequency — please provide these details when requesting a quote.
The cutting method decides pellet shape, dust level, moisture pick-up and how gently the compound is treated at the die. All four are supplied on the same extruder platform, so the choice is made from your material rather than from what the machine can do.
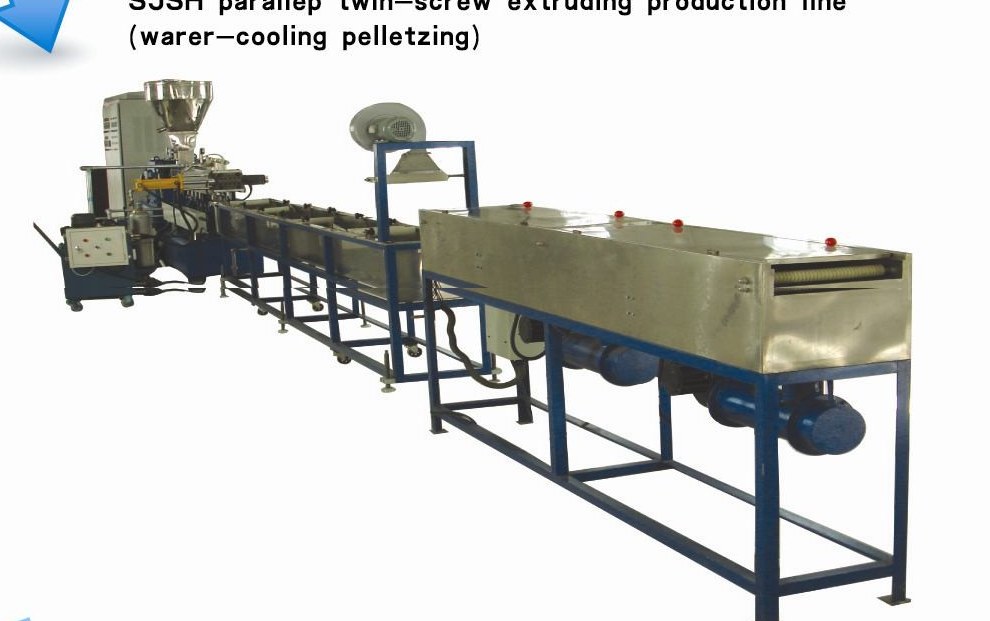
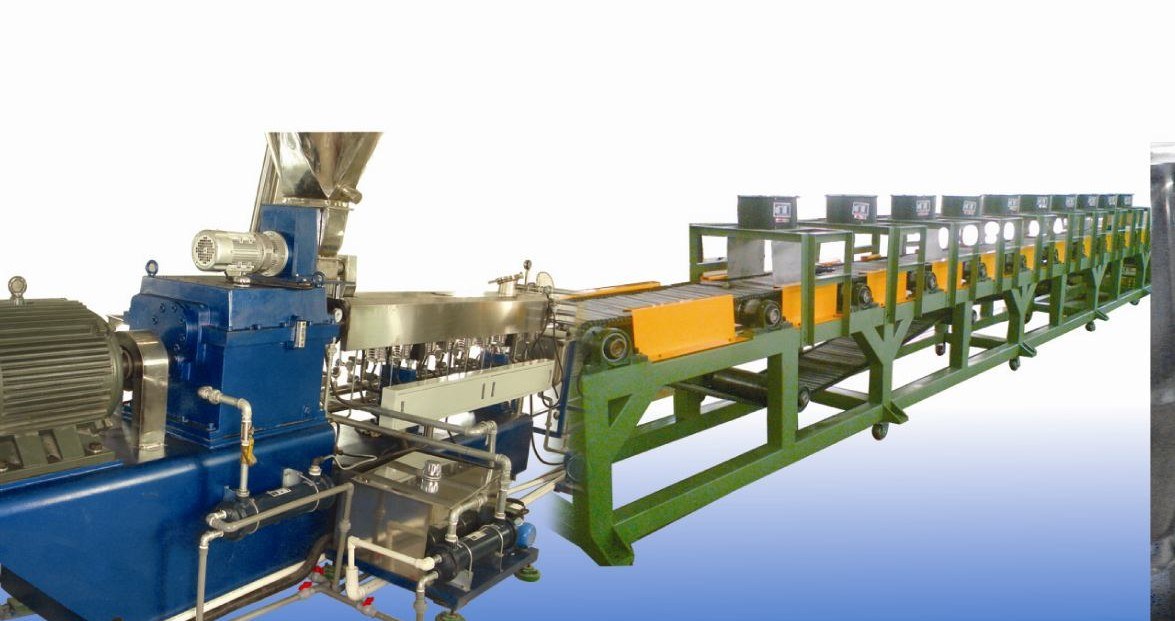
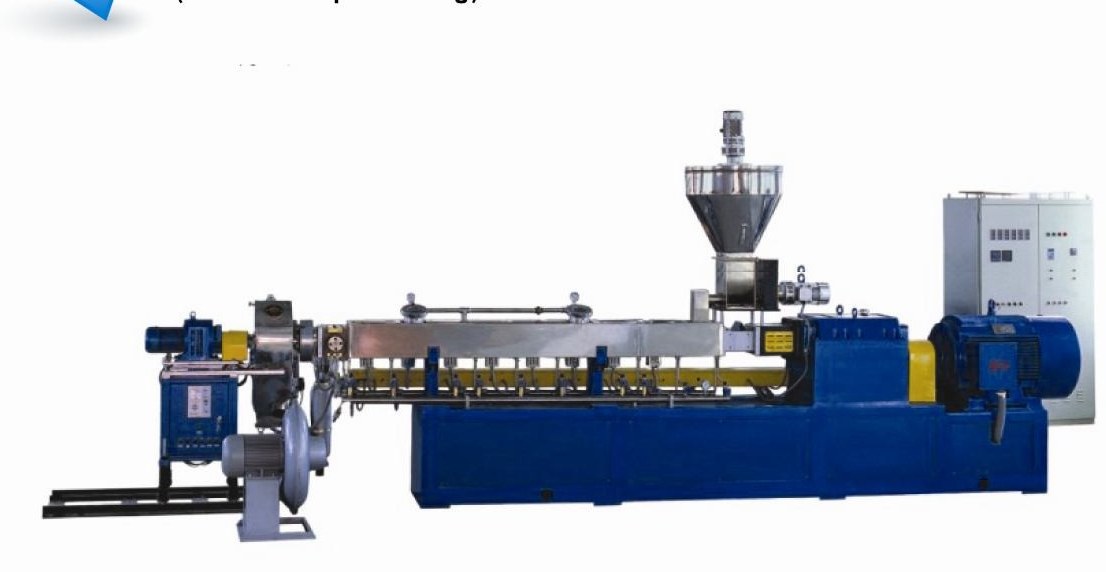
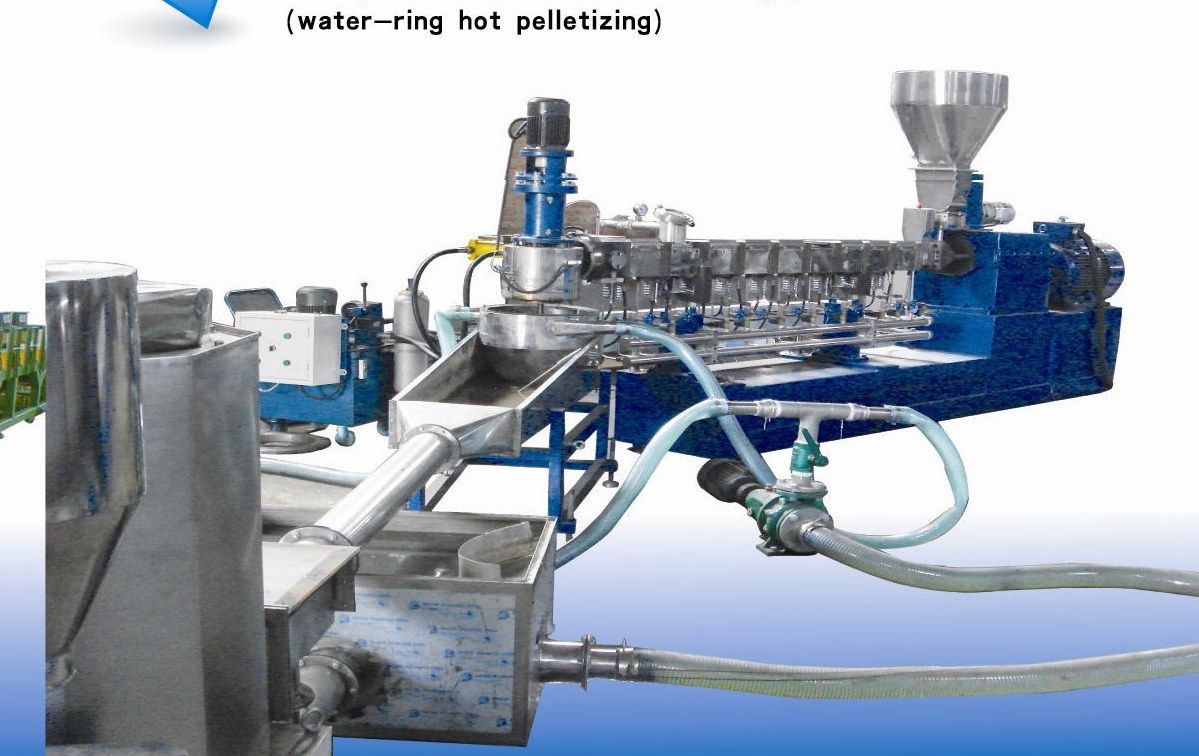
Two further options are supplied where the compound demands them: eccentric fog-jetting hot-face cutting, used on XLPE and peroxide-containing cable compounds where the melt must be cut at low temperature and low pressure, and underwater pelletizing for very high outputs.
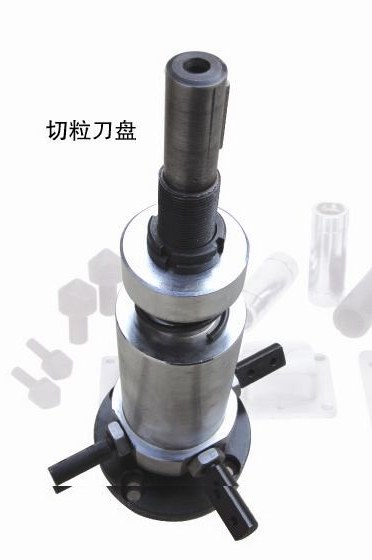
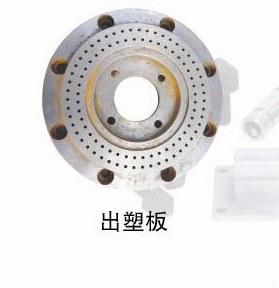
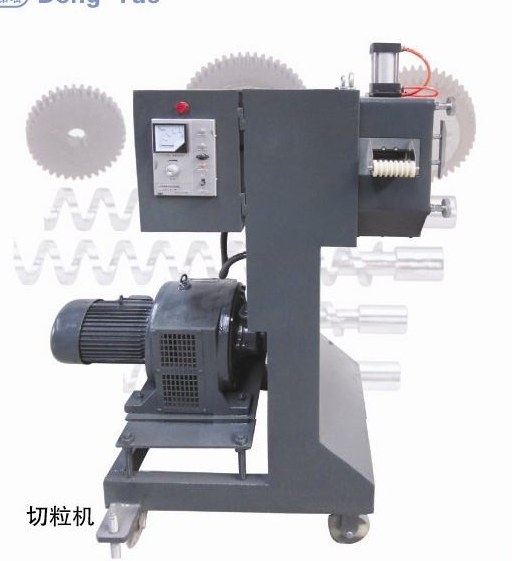
Every line is delivered with a matched control cabinet: one RKC temperature controller per heating zone, EUROTHERM or Japanese variable-frequency speed control on the main drive and feeders, 0–25 MPa melt-pressure monitoring, and interlocks that stop the machine on overpressure or overcurrent and refuse to start without lubrication running. Simulated panel, PLC and PCC control are available on request.