PRODUCTS / TWO-STAGE LINES
A twin-screw first stage combined with a single-screw second stage, decoupling mixing from pressure build-up so heat-sensitive and highly filled compounds can be pelletized gently at low melt temperature.
In the SHJ configuration, a co-rotating twin-screw extruder performs melting, mixing and devolatilization, then discharges into a single-screw extruder that builds pressure and feeds the pelletizer at low, controlled temperature. Separating these functions keeps shear and heat off sensitive formulations and allows very high filler loadings to be pelletized cleanly.
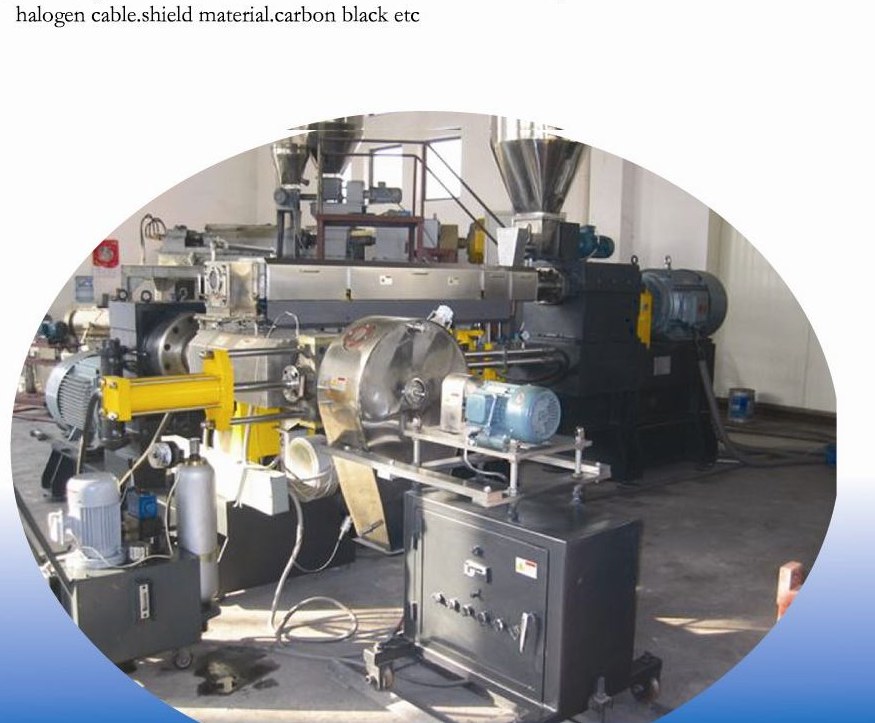
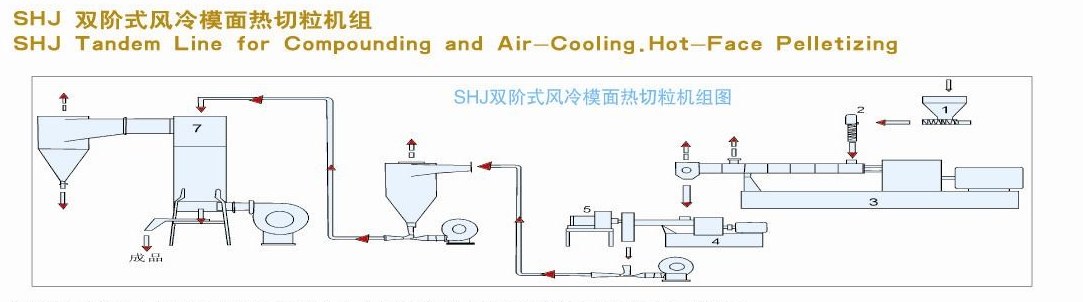
Each SHJ line pairs a high-speed co-rotating twin-screw first stage with a low-speed single-screw second stage, mounted vertically at right angles. Both machines are listed below: D = screw diameter, L/D = length-to-diameter ratio, N = screw speed, P = main motor power, Q = typical output for the complete line.
| Line model | Stage | Machine | D (mm) | L/D | N (r/min) | P (kW) | Q (kg/h) |
|---|---|---|---|---|---|---|---|
| SHJ50-120 | 1 — twin-screw | SJSH50 | 50.5 | 24–48 | 500 | 37–45 | 150–300 |
| 2 — single-screw | SJ120 | 120 | 7–20 | 65–85 | 30–37 | ||
| SHJ65-150 | 1 — twin-screw | SJSH65 | 62.4 | 24–48 | 400–500 | 55–75 | 200–500 |
| 2 — single-screw | SJ150 | 150 | 7–20 | 65–85 | 37–45 | ||
| SHJ75-180 | 1 — twin-screw | SJSH75 | 71 | 24–28 | 400–500 | 90–110 | 300–600 |
| 2 — single-screw | SJ180 | 180 | 7–20 | 65–85 | 45–65 | ||
| SHJ95-200 | 1 — twin-screw | SJSH95 | 93 | 24–28 | 300 | 132–135 | 500–1000 |
| 2 — single-screw | SJ200 | 200 | 7–20 | 85 | 55–75 |
Reference throughput for the compounds the two-stage line is most often specified for, in kg/h.
| Material group | Representative materials | 50/120 | 65/150 | 75/180 | 95/200 |
|---|---|---|---|---|---|
| Heat-susceptible plastics | PVC cable compound, low-smoke zero-halogen, transparent and medical-grade packaging, shoe sole compound | 150–300 | 250–500 | 350–800 | 700–1100 |
| PE peroxide crosslinked cable, silane crosslinked cable, crosslinked piping, PE and EVA shielding compound | 120–250 | 200–450 | 280–600 | 800–1400 |
Catalog reference values — indicative and formulation-dependent. The line is sized against your material, filler loading and required output; screw configuration, venting and pelletizing method are specified per compound.
