Cable Compound and XLPE Production Lines

INSULATION · SHEATHING · XLPE

Cable Compound and XLPE Production Lines

Twin-screw and two-stage systems for cable insulation, sheathing, crosslinkable polyethylene and low-smoke compounds.

Processing challenge

Cable formulations can be highly filled, heat-sensitive or reactive. They require controlled mixing, limited thermal history, effective venting and stable pelletizing.

Recommended equipment approach

The catalogue identifies SHJ two-stage systems for heat- and shear-sensitive compounds and tandem lines for crosslinkable polyethylene. SJSH or DY systems may be selected for other cable compound duties.

Typical materials

  • PVC cable compounds
  • PE cable insulation and sheathing
  • XLPE compounds
  • Low-smoke, low-halogen formulations
  • EVA and carbon-black-containing materials

Pelletizing and downstream

Air-cooled hot-face or other low-water-contact arrangements may be appropriate for water-sensitive materials. Final selection depends on formulation.

Information required for quotation

  • Polymer and crosslinking system
  • Filler and carbon-black content
  • Target output
  • Required pellet moisture and cleanliness
  • Voltage, automation and packaging requirements

Line layouts

XLPE cable compound, tandem line

PE resin, antioxidant and DCP are dosed by loss-in-weight feeder and pump into the twin-screw extruder, then transferred to a single-screw extruder and cut by an eccentric fog-jetting cutter. The low-pressure, short-channel die and low-temperature mixing are what prevent premature crosslinking.
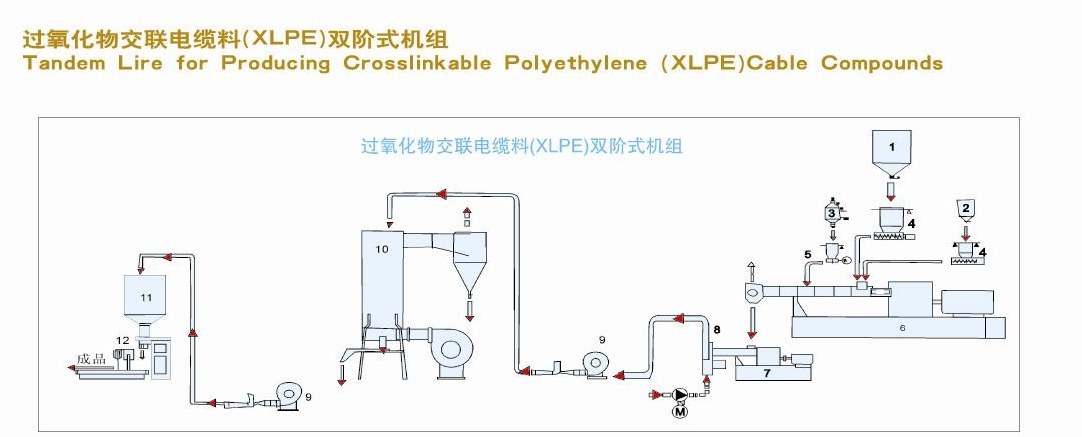
Flow diagram of a tandem line producing crosslinkable polyethylene cable compound with loss-in-weight dosing and eccentric fog-jetting pelletizing
1 PE resin silo, 2 antioxidant silo, 3 DCP tank, 4 loss-in-weight feeder, 5 loss-in-weight pump, 6 twin-screw extruder, 7 single-screw extruder, 8 eccentric cutter, 9 fan, 10 fluidising bed, 11 product container, 12 automatic bagging.

Low-smoke halogen-free and PVC cable compound, SHJ tandem line

For PVC cable compound, low-smoke zero-halogen material and EVA shielding compound, the SHJ tandem line with air-cooled hot-face cutting keeps melt temperature and shear low through the pelletizing stage.
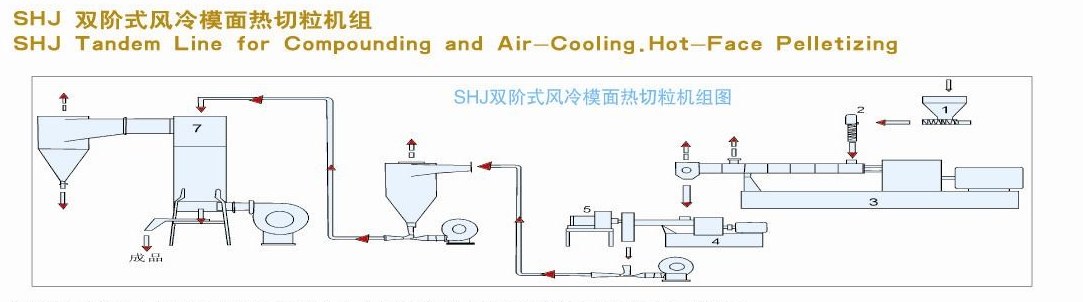
Flow diagram of an SHJ tandem line for compounding and air-cooled hot-face pelletizing of cable compound
1 metering feeder, 2 cramming feeder, 3 twin-screw extruder, 4 single-screw extruder, 5 hot-face cutter with air cooling, 6 cyclone, 7 fluidising bed.

Flame-retardant compound via Banbury mixer

Where aluminium hydroxide or magnesium hydroxide loadings are very high, a Banbury mixer feeding an extruder with eccentric fog-jetting pelletizing handles the filler content that a single compounding pass would struggle with.
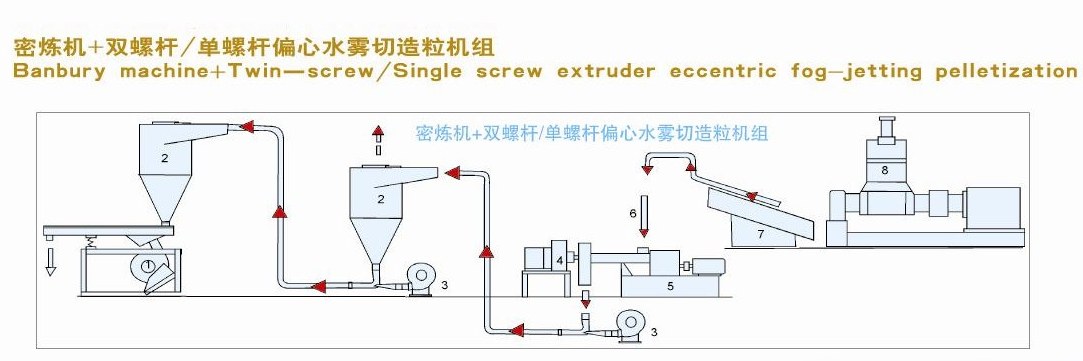
Flow diagram of a Banbury mixer with extruder and eccentric fog-jetting pelletizer for flame-retardant cable compound
Compound50/12065/15075/18095/200
PVC cable, low-smoke zero-halogen, transparent and medical-grade, shoe sole150–300250–500350–800700–1100
PE peroxide and silane crosslinked cable, crosslinked piping, PE and EVA shielding120–250200–450280–600800–1400

Output in kg/h, catalog reference values — confirmed against your formulation.